A metallic floor looks like one person’s artwork. On the day it goes down it is four or five people doing separate jobs at the same moment, and most metallic floors that go wrong go wrong because two of those jobs landed on one set of hands. Stockton crews moving into metallic work tend to ask about pigments first. The better first question is who stands where when the first batch hits the slab.
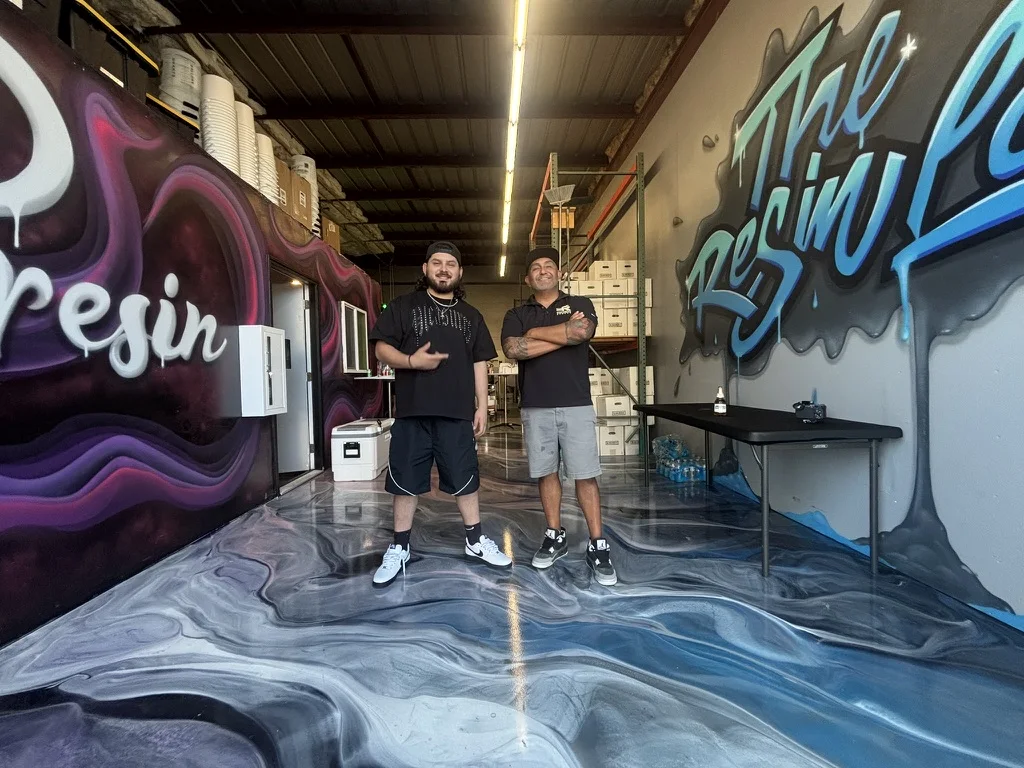
The mixer sets the pace for everyone else
The mixer never touches the floor. Their whole job is turning out identical batches at the rhythm the pour needs, which sounds simple until batch six.
Pigment goes into the clear base and gets dispersed completely before the hardener joins it, in whatever order the system instructions give. Pigment that never fully dispersed shows up on the floor as specks or smears nobody can move out.
Weigh the pigment on a scale for every batch. Scooping by eye can work in one small room and falls apart on a floor that takes a dozen kits, because the color drifts batch to batch and the seams between batches read as stripes under light.
The mixer also stages. Kits laid out in order, pigment weighed ahead into labeled cups, clean pails lined up, drill and paddle ready. When the next batch is called, it should be mixed and moving inside a couple of minutes.
Put your steadiest person here. It is the least visible role on the crew and the one that decides whether the floor ends up one color.
Pouring and spreading are two separate jobs
The pourer takes each batch from the mixer and lays it down in ribbons along the wet edge, in the pattern the crew agreed on before the day started. Pour too far from the edge and you build a lap line where two batches meet after one has already started to set.
Right behind the pourer is the spreader, in spiked shoes, pulling material out to thickness with a gauge rake or notched squeegee and then working it to an even film. Metallic systems usually run heavier than a standard build coat, and thin spots show as dull patches once the pigment settles.
Keeping these roles apart matters most on a big floor. A pourer who stops to spread leaves the next batch sitting in a pail, getting warmer and losing working time. A spreader who stops to pour leaves a rake line drying on the slab.
Both of them watch the wet edge. That line is where the floor either stays continuous or picks up a seam, and it moves across a room faster than a new crew expects.
The movement person works the wet film alone
Behind the spreader comes the person creating the look, rolling, brushing, troweling or spraying to push the pigment into veins and cells. On a well-run pour this is one person, maybe two on a very large floor, and nobody else touches their area.
Every lap shows. A roller that goes back over a spot already worked, a trowel that changes angle halfway across, a knee print, a dropped glove: the finish locks all of it in. Metallic floors record every move made in the wet film, which is why two different hands-on one section rarely blend.
Lighting belongs to this job. Set work lights low and off to the side so the movement person can see ridges, roller marks and dull spots while they are still fixable. Overhead shop lights hide most of it until the floor cures and the owner flips on those same lights.
This person also decides when a section is done, and has to be disciplined about walking away from it. Overworking a good section is one of the fastest ways a nice floor turns muddy. Our page on metallic flooring systems for Stockton covers the material side.
Somebody has to own the clock
The last role is the one crews skip, and often the one that saves the floor. One person watches time and conditions and does very little else.
They track when each batch was mixed, how long it sat in the pail, how long it has been on the floor, and when the working edge starts to stiffen. They call the next batch to the mixer. They know the pot life and working time from the data sheet, and they know both shrink as the room warms.
They also read the room. Slab temperature, air temperature, a roll-up door letting afternoon heat or a breeze across the wet film, dust drifting in from outside. Any of those changes what the movement person can still do.
On a small floor the clock can ride with the mixer. On a floor that takes many batches, hand it to someone with a watch, a notepad and the authority to say stop. A crew with nobody on the clock usually finds out about the problem when the roller starts dragging.
Rehearse the roles before the paid floor
A crew that has never poured a metallic together should not meet its roles for the first time on a customer’s slab.
Practice on boards. Mix a real batch, pour it, spread it and move it on a sample panel with the same people in the same positions you plan to use on the job. You learn how fast the material stiffens in your hands, what your roller does to the pigment, and who on the crew has the eye for movement. That is what the academy side of Exclusive Resin Supply exists for: hands-on time with the systems before a floor is riding on it.
Be honest about readiness. If the crew is still sorting out handoffs, a decorative flake floor is a far more forgiving sell. A broadcast hides many of the small errors a metallic records, and it builds the timing a metallic pour depends on.
When you do book the metallic, walk the roles one more time the day before. Five minutes on who stands where saves a lot of grinding.
Staffing questions from crews new to metallics
How many people does a metallic pour need?
For most garage and shop floors, plan on four: a mixer, a pourer, a spreader and one person doing the movement, with the mixer or pourer also watching the clock on smaller jobs. Larger floors often add a dedicated clock person or a second spreader. Fewer than four usually means somebody is doing two jobs at the moment both need full attention.
Can one person mix and pour on a small floor?
In a small room with only a few batches, some crews make it work. The risk is time, since every minute the pourer spends mixing is a minute the wet edge sits. If you combine the roles, weigh every pigment cup and stage every kit before the first batch goes in, so each mix takes as little time as possible.
Where can a crew practice metallic work before a customer job?
The academy side of Exclusive Resin Supply exists for this. Crews can work the systems hands-on, with the owner, on boards before a paid floor depends on it. Call the bench and tell us what the crew has poured so far, and we will talk through what training makes sense for the metallic work you want to sell.
Before the first paid metallic, write a name next to each job on pour day: mixer, pourer, spreader, movement and clock. If one name shows up twice, that is the gap to close, with another hand or with a few boards at the academy first. Call (209) 208-4656 with the crew you have, or describe the room and the look, and we will size the batches to the people pouring them.